Testing & Quality Control
Every rig, and the standard it runs to.
Most sole factories tell you they have testing equipment. That is not the useful sentence. The useful sentence is which standard each machine certifies against, because that is what decides whether our numbers match the ones your laboratory produces.
| Property | Equipment on site | Standard |
|---|---|---|
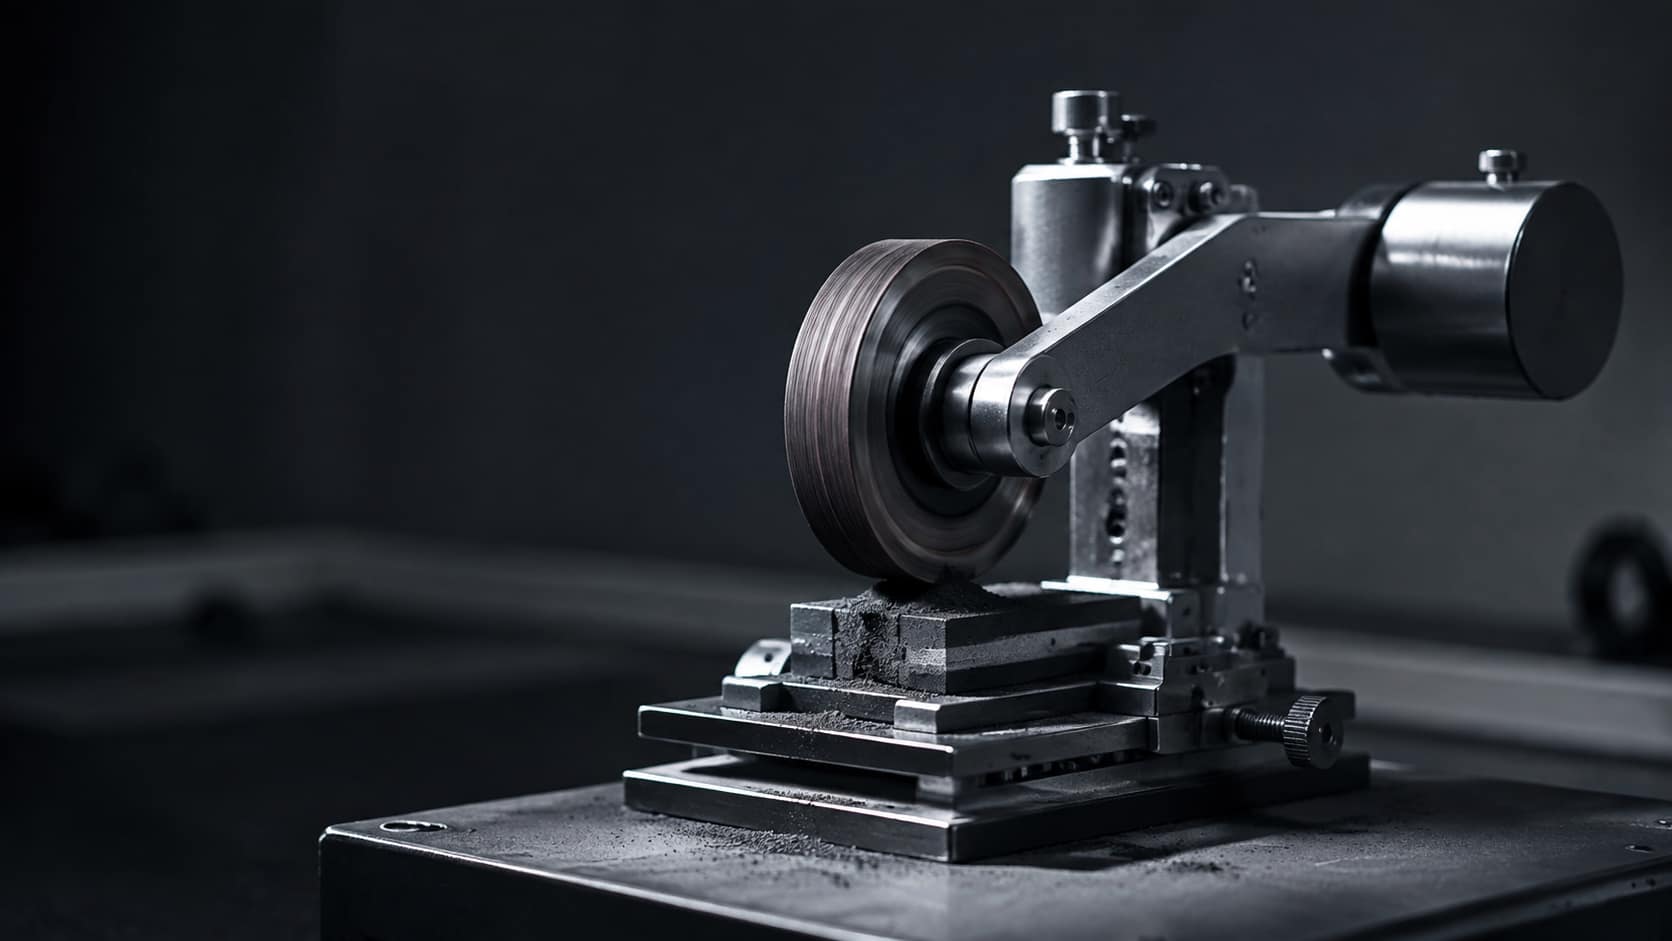
| Abrasion resistance | DIN abrasion tester | ISO 4649 method A · DIN EN 12770 · SATRA TM174 |
| A specimen is run against a rotating abrasive sheet and the result comes back as volume loss in mm³, so a lower number is the harder-wearing compound. Method A is the rotating-specimen variant, which matters when your laboratory compares its figure with ours. | ||
| Footwear slip resistance | Slip resistance tester | SATRA TM144 · ISO 13287 · ASTM F2913 |
| A whole-shoe test, not a material test: the result is a coefficient of friction on a defined surface with a defined contaminant, forward heel and flat, so the tread pattern is measured along with the compound. Change the tread and this number changes. | ||
| Tensile strength & elongation | Tensile tester | ISO 37 · SATRA TM410 series |
| Reported as strength in MPa and elongation at break as a percentage. The pair reads together: high strength with low elongation is a compound that will crack rather than flex, which is what shows up at a flex groove long before it shows up on the outsole face. | ||
| Density | Density tester | ISO 2781 |
| Grams per cubic centimetre, and the figure that turns a drawing into a shipping weight and a unit cost. It is also the fastest check that a foamed batch matches the one signed off, because a density drift shows up before any hardness change does. | ||
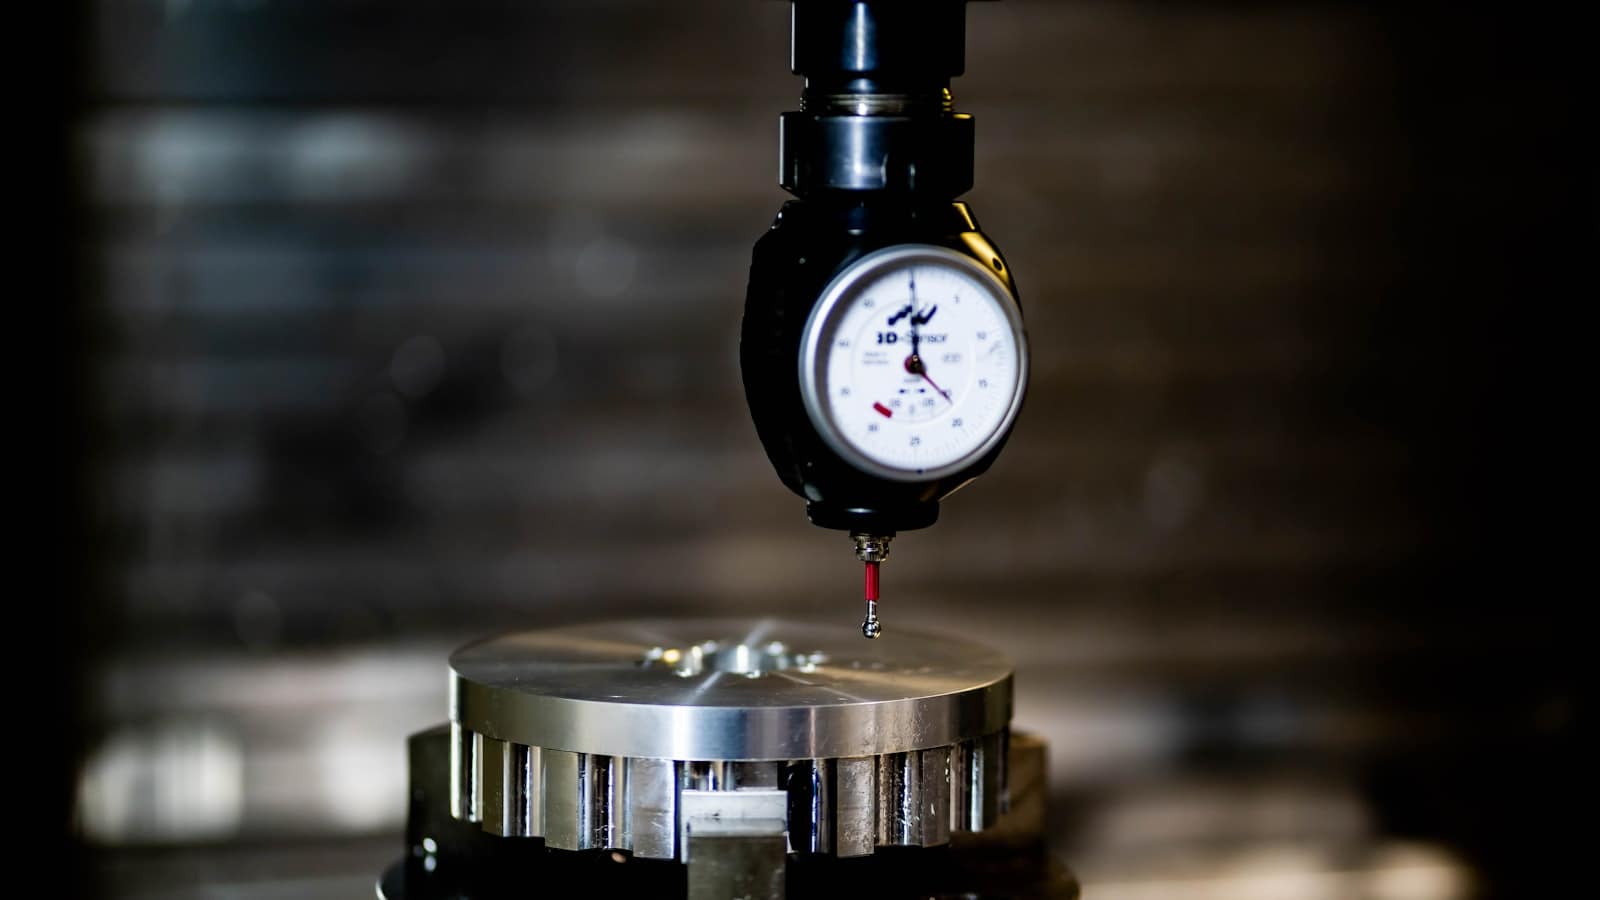
| Hardness | Durometer | SATRA TM205 (Shore A / Shore C) |
| Shore points, on the scale that belongs to the material: Shore A for rubber and TPR, Shore C for EVA. The scales do not convert, so a figure quoted without its scale cannot be checked. Measured on the finished sole, not on a slab. | ||
| Cure characteristics | Rheometer | ISO 6502 |
| A cure curve for the compound before it reaches a mould, giving scorch and optimum cure time. It is what sets the press cycle, and the reason a repeat order behaves like the sample: the same curve, the same cycle, the same sole. | ||
| Thermal ageing & low temperature | Constant-temperature chamber | Conditioning per customer protocol |
| Conditioning rather than a test in itself: specimens are held at temperature for a set time, then re-tested on the rigs above so the numbers are before-and-after. Cold conditioning is the one to ask for on a TPR sole and on any winter programme. | ||
| Non-marking / scuff | Scuff-mark tester | Referenced to SATRA TM223 |
| Whether the sole transfers colour to a floor, assessed against the reference method. This is a hall, court and hospitality requirement that arrives late and cannot be solved by tooling — it is a compound and pigment decision taken before the mould is cut. | ||
| Shrinkage & yellowing | Shrinkage & yellowing tester | No single common standard; run to brand protocol |
| Dimensional change after moulding, and colour shift on ageing. Shrinkage is why a mould is cut oversize by a known factor per material; yellowing is why a white or pastel sole is checked on ageing rather than only on the day it is signed off. | ||
Sent to an external laboratory
Not every test belongs in a sole factory. These we book with an accredited lab and return with the report, rather than claim in-house.
Certification
Scope certificate GRC06675, valid to 24 June 2027, covering recycled-content handling and chain of custody. Scope certificates expire, so we send the current one rather than a logo. No public register link here yet: we have not been able to locate this certificate in a scheme register, so ask us for the original and check it with the issuing body.
Original on request
Certificate ESTS-COC-260974, licence code FSC-C230627, issued by ESTS and valid 21 July 2026 to 20 July 2031. The scope covers manufacturing and sales of footwear (FSC product category N7.1.4) as FSC Mix, under FSC-STD-40-004, covering traceability for certified natural rubber through to the finished sole.
Verify in the public register →Independent laboratory test reports issued per programme. Current reports available on request.
Original on request
Questions buyers ask about this
What can you test on site, and what goes to a laboratory?
Eight rigs on site cover DIN abrasion, footwear slip resistance, tensile and tear, density, vulcanisation cure, scuff marking, shrinkage and yellowing, and conditioned thermal ageing. Ross flex, outsole-to-midsole peel, EN ISO 20345 safety footwear work and chemical compliance are booked with an accredited external laboratory and come back as reports.
Do you hold ISO 9001?
No. Hongcheng holds FSC Chain of Custody (certificate ESTS-COC-260974, licence code FSC-C230627, valid to 2031-07-20, checkable in the FSC public register) and GRS 4.0 (scope certificate GRC06675, valid to 2027-06-24), and does not hold an ISO 9001 certificate. We would rather state that plainly than let a supplier questionnaire discover it.
Is safety footwear still marked SRA, SRB or SRC?
No. EN ISO 20345:2022 withdrew those markings. Basic slip resistance became a mandatory requirement for all safety footwear, and SR now marks the enhanced test. Supplier sites still advertising "SRC rated" soles are quoting a superseded scheme.
Need the test data for a specific compound?
Tell us the sole system and the standard you certify to. We send the in-house data and book anything else with an accredited laboratory.